7 Benefits of Manufacturing Inventory Management Software
7 Benefits of Manufacturing Inventory Management Software
Imagine this: Your production team is ready to start manufacturing a large order. The machines are running, employees are prepared, and everything seems to be going according to plan. But suddenly, someone realizes a critical raw material is missing. Now what? Production stops, deliveries get delayed, and your team scrambles to figure out what went wrong.
Sounds frustrating, right?
Unfortunately, situations like these are common when manufacturers rely on spreadsheets, paperwork, or outdated inventory processes. That's where manufacturing inventory management software comes into play. Instead of constantly chasing stock updates and worrying about missing materials, manufacturers can track inventory, plan production, and keep operations moving smoothly.
But that's just the beginning. Let's explore seven benefits that make this software a valuable investment for manufacturing businesses.
What Is Manufacturing Inventory Management Software?
Think of manufacturing inventory management software as the control center for everything moving in and out of your production facility. It helps businesses monitor raw materials, work-in-progress inventory, finished products, and stock movements from one centralized system.
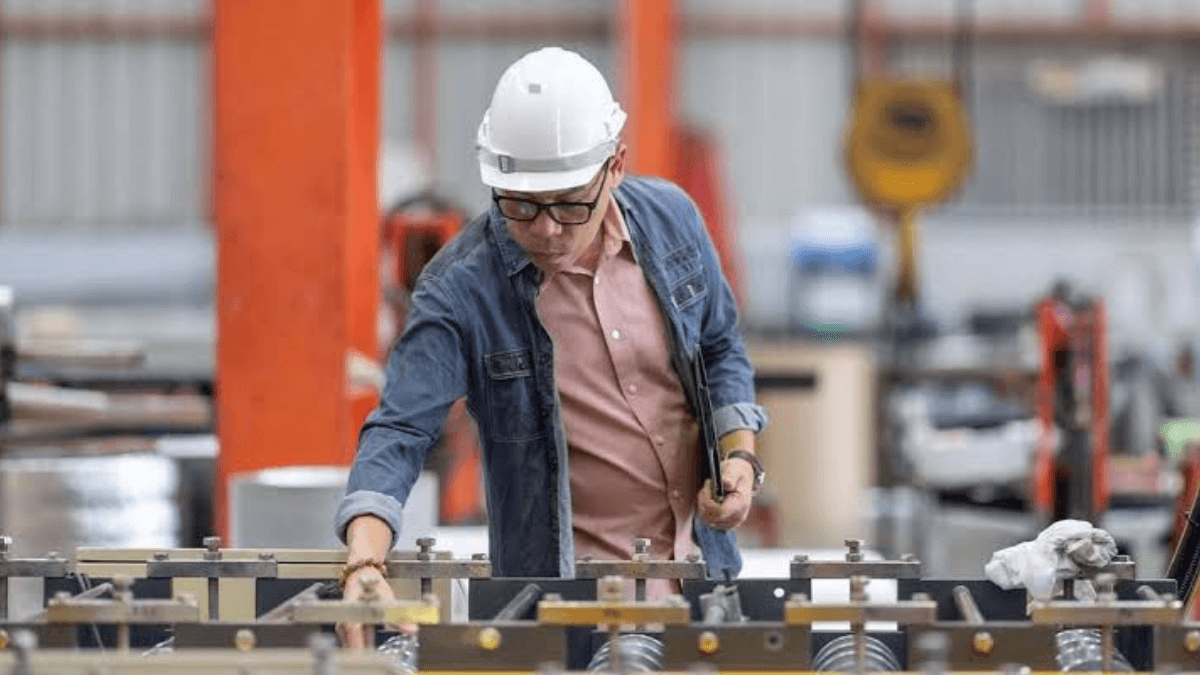
Unlike basic stock management tools, manufacturing-focused software can connect inventory information with production schedules, purchasing activities, and material requirements. For example, suppose your company manufactures office furniture. You need wood, screws, fabric, metal frames, and packaging materials to complete an order.
Without a proper system, keeping track of each component can become a headache. With the right inventory control system, you can monitor available materials, identify shortages, and determine when it's time to reorder.
The goal is simple: Make inventory management less complicated and manufacturing more efficient.
1. Know Exactly What's in Stock
Ever spent hours searching for something you were sure was sitting in your warehouse? It's like looking for your car keys, except those missing keys could delay an entire production line.
One of the biggest benefits of manufacturing inventory management software is improved inventory visibility. Instead of guessing how much material is available, your team can access updated stock information from a single platform.
With reliable inventory tracking software, manufacturers can:
- Monitor raw materials and finished products.
- Track stock movements between warehouse locations.
- Identify materials that are running low.
- Reduce errors caused by manual recordkeeping.
For businesses managing hundreds or thousands of components, that visibility can make everyday operations significantly easier.
2. Prevent Costly Production Delays
Picture a bakery preparing 5,000 packaged cookies for a major retailer. Everything is ready until the production manager discovers there isn't enough packaging material to complete the order.
The ingredients are available, the machines are working, but production still cannot finish on schedule. That's the problem with poor inventory planning. Sometimes, one missing component is all it takes to interrupt an entire operation.
Manufacturing inventory management software helps reduce these situations by monitoring material availability and supporting timely purchasing decisions. Some systems can even generate low-stock alerts or calculate material requirements based on upcoming production orders.
The result? Fewer unexpected shortages, better scheduling, and a production team that can focus on manufacturing rather than solving avoidable inventory problems.
3. Reduce Inventory Costs and Unnecessary Spending
Having extra inventory might sound like a smart safety measure. After all, isn't it better to have too much than too little?
Not necessarily.
Excess inventory ties up working capital, consumes storage space, and increases the risk of damage or obsolescence.
Imagine a manufacturer ordering twice as many electronic components as needed. Those components could sit unused for months while valuable money remains locked in warehouse shelves.
A well-configured inventory control system helps businesses understand purchasing patterns, maintain appropriate stock levels, and reduce unnecessary orders.
It can also support better decisions about which materials should be reordered frequently and which should be purchased only when required.
Instead of filling warehouses with materials that might be used someday, manufacturers can make purchasing decisions based on actual operational needs.
4. Improve Accuracy and Reduce Human Errors
Let's face it. Nobody enjoys manually entering hundreds of inventory numbers into spreadsheets. And even the most careful employee can accidentally type 500 instead of 50. That single mistake could lead to unnecessary purchasing, inaccurate inventory reports, or production scheduling problems.
Manufacturing inventory management software can reduce manual data entry through automated stock updates, barcode scanning, and integrated workflows. For example, when warehouse employees scan materials as they enter or leave storage, compatible inventory tracking software can record those transactions immediately.
This reduces dependence on handwritten records and disconnected spreadsheets. Of course, software doesn't eliminate every mistake. Employees still need accurate processes and proper training. However, automation can significantly reduce opportunities for common recording errors.
5. Make Smarter Decisions With Real-Time Data
Would you rather make an important business decision based on yesterday's spreadsheet or current inventory information?
The answer seems obvious.
Manufacturing inventory management software provides useful insights into inventory levels, stock movements, consumption patterns, and purchasing activity.
Depending on the platform, manufacturers can generate reports showing which materials are used most frequently, which products are moving slowly, and where inventory costs are increasing.
Consider a company manufacturing kitchen appliances.
After reviewing inventory reports, the purchasing manager notices that one particular component consistently experiences shortages during seasonal demand increases.
With that information, the company can adjust purchasing schedules before the next busy season. Instead of constantly reacting to problems, businesses can start anticipating them. And that's what makes data valuable: It turns information into better decisions.
6. Strengthen Coordination Between Departments
Manufacturing isn't a one-person show.
Purchasing teams order materials, warehouse employees manage stock, production teams assemble products, and sales departments communicate delivery expectations to customers.
Now imagine each department working from a different spreadsheet. Sounds like a recipe for confusion. A centralized inventory control system can improve coordination by giving authorized teams access to consistent inventory information.
For example, when the sales department receives a large order, production planners can review available materials while purchasing teams identify additional supply requirements.
Everyone works with the same information rather than exchanging endless emails asking, "Do we have enough stock?" This improves communication, reduces duplicated work, and helps departments coordinate more effectively.
When information moves smoothly between teams, manufacturing operations become easier to manage.
7. Support Business Growth Without Inventory Chaos
Running a small manufacturing operation with a few products is one thing. Managing multiple warehouses, hundreds of suppliers, and thousands of inventory items? That's a completely different challenge. As businesses grow, manual inventory processes often become difficult to maintain.
More products mean more materials to track. More customers mean more orders to fulfill. More warehouse locations mean more opportunities for stock discrepancies. Scalable manufacturing inventory management software helps businesses handle that growing complexity.
Depending on the solution, companies can add warehouse locations, expand product catalogs, manage more transactions, and integrate inventory operations with other business systems. For example, a manufacturer expanding from one production facility to three can benefit from centralized inventory visibility across locations.
Instead of managing separate records for every facility, teams can monitor stock levels and coordinate material transfers more efficiently. Growth should create new opportunities, not endless inventory headaches.
How to Choose the Right Manufacturing Inventory Management Software
Not every inventory management solution is designed for manufacturing. Some platforms focus primarily on retail stock, while others include specialized features for managing production materials and manufacturing workflows.
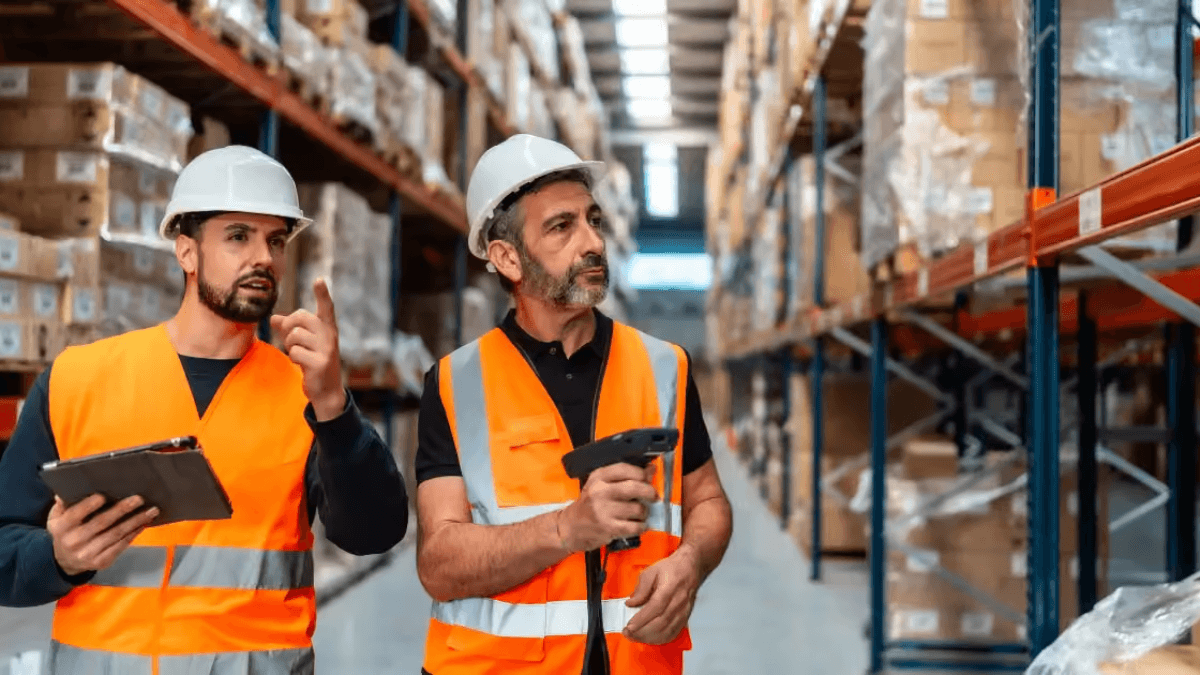
Before selecting software, consider these important capabilities:
- Real-time inventory tracking: Monitor material availability and stock movements.
- Production integration: Connect inventory data with manufacturing orders and material requirements.
- Automated alerts: Receive notifications when inventory reaches predefined reorder levels.
- Reporting and analytics: Understand purchasing patterns and inventory performance.
- Scalability: Support additional products, warehouses, and operational complexity as your business expands.
Also consider ease of use, implementation costs, employee training, and compatibility with your existing accounting or ERP systems.
The best software isn't necessarily the one with the longest feature list. It's the one that solves your business's actual inventory challenges.
Final Thoughts
Manufacturing is complicated enough without constantly worrying about missing materials, inaccurate stock records, or unexpected production interruptions. That's why manufacturing inventory management software can make such a meaningful difference.
From improving inventory accuracy and reducing unnecessary costs to strengthening teamwork and supporting business growth, the right system helps manufacturers operate with greater confidence and control.
Whether you're managing a small production facility or expanding into multiple warehouses, investing in effective inventory management can make your daily operations more organized and predictable. Because at the end of the day, successful manufacturing isn't just about producing more. It's about having the right materials, in the right place, at the right time.
Recent Posts
Aroopa Apps is an AI-powered low-code/no-code platform for building custom business apps, automating workflows, and streamlining business processes faster and smarter.
New Jersey
Aroopa, Inc
111 Union Valley Rd, Suite 206, Monroe Township, NJ 08831
India
Aroopa Technologies Private Limited
No.2, Padmavathi Nagar,
Agraharam Road, Korattur,
Chennai 600076
Aroopa Apps is now on Android & iOS!


Subscribe to Our Newsletter
Copyright © Aroopa Apps 2026